
The Benefits of Using 3PE Coated Steel Pipe for Underground Applications
2025-02-14
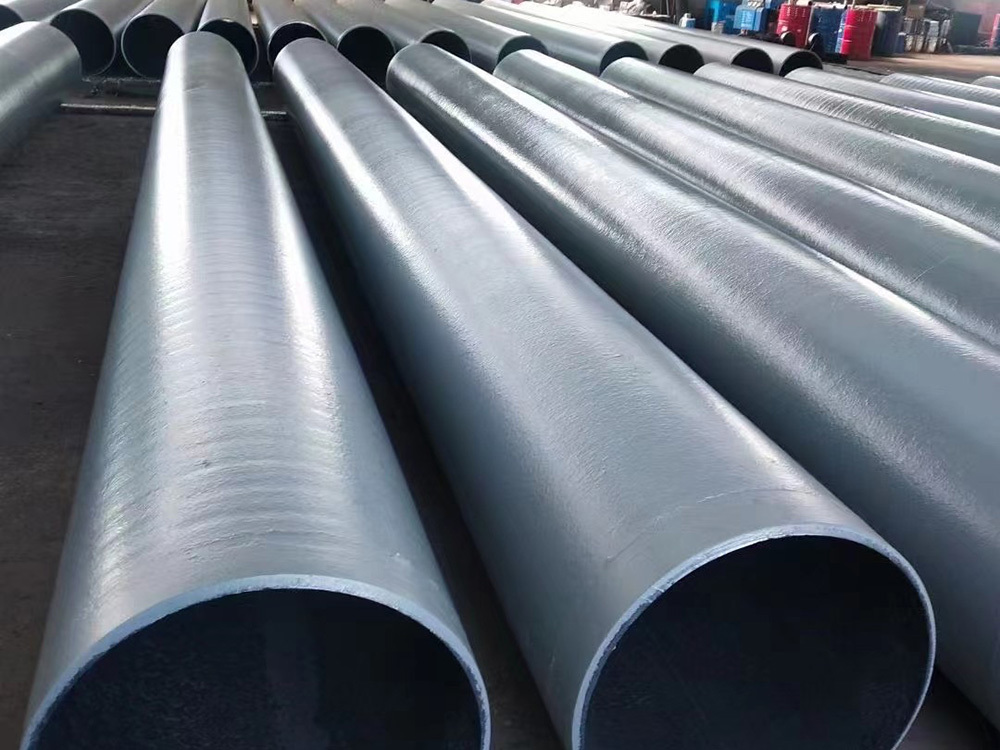
The Benefits of Using 3PE Coated Steel Pipe for Underground Applications
Table of Contents
- 1. Introduction to 3PE Coated Steel Pipe
- 2. What is 3PE Coating?
- 3. Advantages of 3PE Coated Steel Pipes
- 4. Exceptional Corrosion Resistance
- 5. Longevity and Durability
- 6. Cost-Effectiveness of 3PE Coated Steel Pipes
- 7. Key Applications in Underground Construction
- 8. Sustainability and Environmental Impact
- 9. Frequently Asked Questions (FAQs)
- 10. Conclusion
1. Introduction to 3PE Coated Steel Pipe
In the realm of construction and infrastructure, choosing the right materials is paramount. Among these, **3PE coated steel pipes** have emerged as a preferred choice for underground applications. These pipes not only offer structural integrity but also boast enhanced protection against environmental factors. This article dives into the numerous benefits of using 3PE coated steel pipes, particularly when buried underground, and how they can serve the construction industry effectively.
2. What is 3PE Coating?
**3PE**, or **Three-Layer Polyethylene** coating, is a sophisticated protective system designed for steel pipes. This coating comprises three distinct layers:
1. **Epoxy Primer**: This layer provides excellent adhesion and corrosion resistance.
2. **Adhesive Layer**: This layer binds the epoxy primer to the outer polyethylene layer.
3. **Polyethylene Layer**: This final layer offers additional protection against mechanical damage and moisture.
Each layer is meticulously applied to ensure that the steel pipe is shielded from corrosive elements, making it ideal for underground usage.
3. Advantages of 3PE Coated Steel Pipes
The adoption of 3PE coated steel pipes comes with a multitude of advantages that enhance their appeal in the construction industry. Key benefits include:
- **Superior Protection**: The layered structure of the 3PE coating grants exceptional defense against corrosion and physical damage.
- **Long Service Life**: Enhanced durability ensures that these pipes can withstand harsh underground conditions for extended periods.
- **Reduced Maintenance Costs**: The protective features minimize the need for frequent repairs or replacements, making them a financially sound choice.
4. Exceptional Corrosion Resistance
One of the most significant threats to any underground piping system is **corrosion**. Factors such as moisture, soil composition, and chemical exposure can severely compromise unprotected steel pipes. However, the 3PE coating provides an unmatched barrier:
- **Chemical Resistance**: The epoxy and polyethylene layers are resistant to many chemicals found in soil, ensuring that the integrity of the steel remains intact.
- **Moisture Shielding**: The impermeable nature of the coating prevents moisture ingress, a primary cause of corrosion.
5. Longevity and Durability
Longevity is a critical consideration when selecting materials for underground applications. 3PE coated steel pipes are engineered for **durability**:
- **Impact Resistance**: The polyethylene layer not only protects against corrosion but also against physical impacts, which can be prevalent due to soil movement.
- **Temperature Resistance**: These pipes can withstand a range of temperatures, further extending their lifespan in varying environmental conditions.
6. Cost-Effectiveness of 3PE Coated Steel Pipes
Investing in **3PE coated steel pipes** can lead to significant savings over time:
- **Low Maintenance**: The protective qualities of the coating lead to decreased maintenance needs, reducing overall operational costs.
- **Extended Lifespan**: The durability translates to fewer replacements, allowing for budget allocation towards other essential construction needs.
7. Key Applications in Underground Construction
The versatility of 3PE coated steel pipes makes them suitable for a variety of underground applications, including:
- **Water and Wastewater Systems**: Their resistance to corrosion and chemicals is crucial in protecting water supply and sewage systems.
- **Oil and Gas Pipelines**: The ability to withstand harsh environmental conditions makes them ideal for oil and gas transport.
- **Mining and Industrial Use**: Heavy-duty applications benefit from the impact resistance and durability of 3PE coated pipes.
8. Sustainability and Environmental Impact
Using 3PE coated steel pipes aligns with sustainable construction practices:
- **Resource Efficiency**: Their longevity reduces waste associated with frequent replacements, contributing to a lower carbon footprint.
- **Recyclability**: Steel is inherently recyclable, allowing for reduced environmental impact at the end of the pipe's lifecycle.
9. Frequently Asked Questions (FAQs)
What is the lifespan of 3PE coated steel pipes?
**3PE coated steel pipes** can last anywhere from 30 to 50 years or more, depending on environmental conditions and maintenance practices.
Are 3PE coated pipes suitable for all soil types?
Yes, **3PE coated pipes** are designed to withstand various soil conditions, including those that are corrosive or contain high moisture levels.
How do 3PE coated pipes compare to traditional steel pipes?
3PE coated pipes offer superior corrosion resistance and durability compared to traditional steel pipes, resulting in lower maintenance costs and longer service life.
Can 3PE coated pipes be used for high-temperature applications?
While **3PE coated pipes** are suitable for a range of temperatures, it's essential to verify specific temperature tolerances based on application needs.
Are there any environmental concerns with using 3PE coated pipes?
No significant environmental concerns exist, as both the coating materials and steel can be recycled, and their long lifespan reduces waste.
10. Conclusion
In summary, the benefits of using **3PE coated steel pipes** for underground applications are numerous and compelling. Their exceptional corrosion resistance, longevity, cost-effectiveness, and suitability for various applications make them a wise choice for modern construction projects. By opting for 3PE technology, construction professionals can ensure the durability and reliability of their underground piping systems while also promoting sustainable practices in the industry. In a world where infrastructure integrity is paramount, 3PE coated steel pipes stand out as a robust solution for the challenges faced in underground applications.
Blog

Understanding Polyurethane Direct Buried Insulation Pipes: A Comprehensive Guide
Polyurethane direct buried insulation pipes are specialized piping systems designed to transport fluids while minimizing heat loss. These pipes are particularly valuable in industries where temperature maintenance is crucial, such as metallurgy and energy. The insulation properties of polyurethane make these pipes ideal for applications that require a high level of thermal efficiency.
One of the p

Contact information
200 metres west of the south side of the intersection of Hope Avenue and Fenqi Road, Xindian Town, Mengcun Hui Zuzizhixian, Cangzhou City, Hebei Province, China


Message feedback
If you are interested in our products, please leave your email and we will contact you as soon as possible. Thank you!